


Irregular cutting edges of stamping dies, carbide punches, progressive dies for automotive connectors, silicon-steel laminations for small motors, and powder metallurgy die inserts are widely used in automotive electronics, home appliance hardware, instrumentation, and motor industries. The machining of these workpieces presents significant challenges: after hardening, the hardness generally reaches HRC58-62, which is beyond the capacity of ordinary milling and grinding tools; complex irregular profiles, narrow slots and tiny splines are inefficient and inaccurate when produced by drilling; carbide die inserts require expensive form grinding wheels; thin-wall and elastic workpieces deform under cutting force. The ANTISHICNC DK7735 high-speed wire EDM machine, based on high-frequency pulse spark erosion, drives a 0.12-0.20mm molybdenum wire along the programmed contour on a CNC cross table, cutting any complex profile in hardened steel, carbide, copper and aluminum in a single setup, stably enabling multi-variety, small-batch production of stamping dies, progressive dies and irregular parts.
Recently, a precision hardware stamping component manufacturer in Ho Chi Minh City, Vietnam, contacted the Shanghai ANTISHICNC team. The client needed to machine the hardened-steel irregular cutting edges of an automotive connector progressive die and carbide punches, with a maximum workpiece thickness of 80mm. The requirements for cutting-edge dimensional accuracy, kerf consistency and surface roughness were stringent. Considering the workpiece thickness, profile complexity and multi-variety small-batch production, our engineers recommended the DK7735 high-speed wire EDM machine as the optimal machining solution.
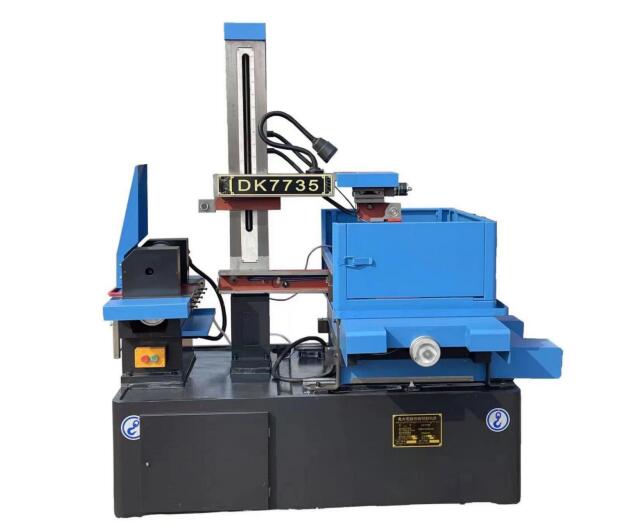
The ANTISHICNC DK7735 is equipped with a high-precision cross table driven by precision ball screws, and a CNC system with automatic wire-wear compensation. The high-frequency pulse power supply can switch discharge parameters for hardened steel, carbide, copper and aluminum. The dual-speed wire drive runs stably, with molybdenum wire recycled through a filtered working-fluid system. The single-side spark gap is about 0.01mm, machining accuracy reaches ±0.015mm, and the best surface roughness Ra ≤ 2.5μm. It generates no cutting force against HRC60+ hardened steel, carbide inserts and thin-wall workpieces, avoiding macroscopic deformation, and eliminating the need for expensive form mills or form grinding wheels. It is perfectly suited for hardened irregular die edges, carbide punches, narrow slots and thin-sheet machining scenarios.
The following are the machine parameters.
| No. | Item | Unit | Technical parameters |
| 1 | Table travel (X×Y) | mm | 320×400 |
| 2 | Max. machining size of workpiece (L×W×H) | mm | 600×400×100 |
| 3 | Max. workpiece weight | kg | 500 |
| 4 | Max. cutting thickness | mm | 100 |
| 5 | Wire diameter (molybdenum) | mm | Φ0.12~0.20 |
| 6 | Max. cutting efficiency | mm²/min | 100 |
| 7 | Best surface roughness | μm | Ra ≤ 2.5 |
| 8 | Machining accuracy | mm | ±0.015 |
| 9 | Single-side spark gap | mm | 0.01 |
| 10 | Wire speed | m/s | 11 |
| 11 | Max. table loading | kg | 500 |
| 12 | Pulse power supply | kW | 2 |
| 13 | Working fluid | — | Emulsion |
| 14 | CNC system | — | High-speed wire EDM CNC |
| 15 | Wire wear compensation | — | Automatic |
| 16 | Power supply | V/Hz | 380/50 |
| 17 | Machine outline dimensions (L×W×H) | mm | 1600×1300×1700 |
| 18 | Net weight / gross weight (approx.) | kg | 1500/1700 |
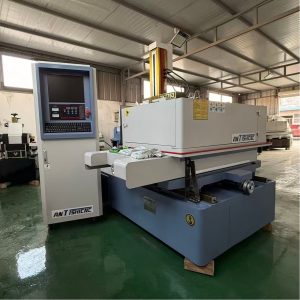
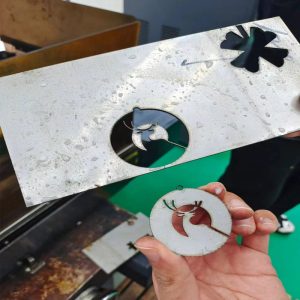
Machine tool appearance & machining display
| Machine appearance | Processed finished products |
 |
 |
ANTISHICNC’s technical team addressed the customers’ challenges in machining hardened-steel irregular die edges and carbide punches by providing pulse parameter reference tables for different thicknesses and materials, molybdenum-wire selection guidance, and working-fluid mixing and replacement schedules. After equipment delivery, all customer samples passed tests for cutting-edge dimensions, kerf consistency and surface roughness, and the equipment is now being used for stable multi-variety production of automotive connector dies and carbide punches.
If you have machining needs for irregular stamping die edges, carbide punches, progressive die cores, motor silicon-steel laminations, narrow slots, thin sheets, and complex profiles in hardened materials, please contact Shanghai ANTISHICNC: contact@antsmachine.com.
We specialize in high-speed wire EDM machines, medium-speed wire EDM machines, CNC lathes and vertical machining centers. We have successful case studies of irregular-profile machining in the automotive die, automotive connector, hardware stamping and motor industries. Our engineers provide one-on-one customized equipment and complete cutting process solutions based on workpiece drawings, material, thickness and precision requirements.
Keywords: High-speed wire EDM, DK7735, hardened steel machining, carbide punch, stamping die machining, progressive die cutting edge